How to Install Metal O-Rings for High-Pressure Systems
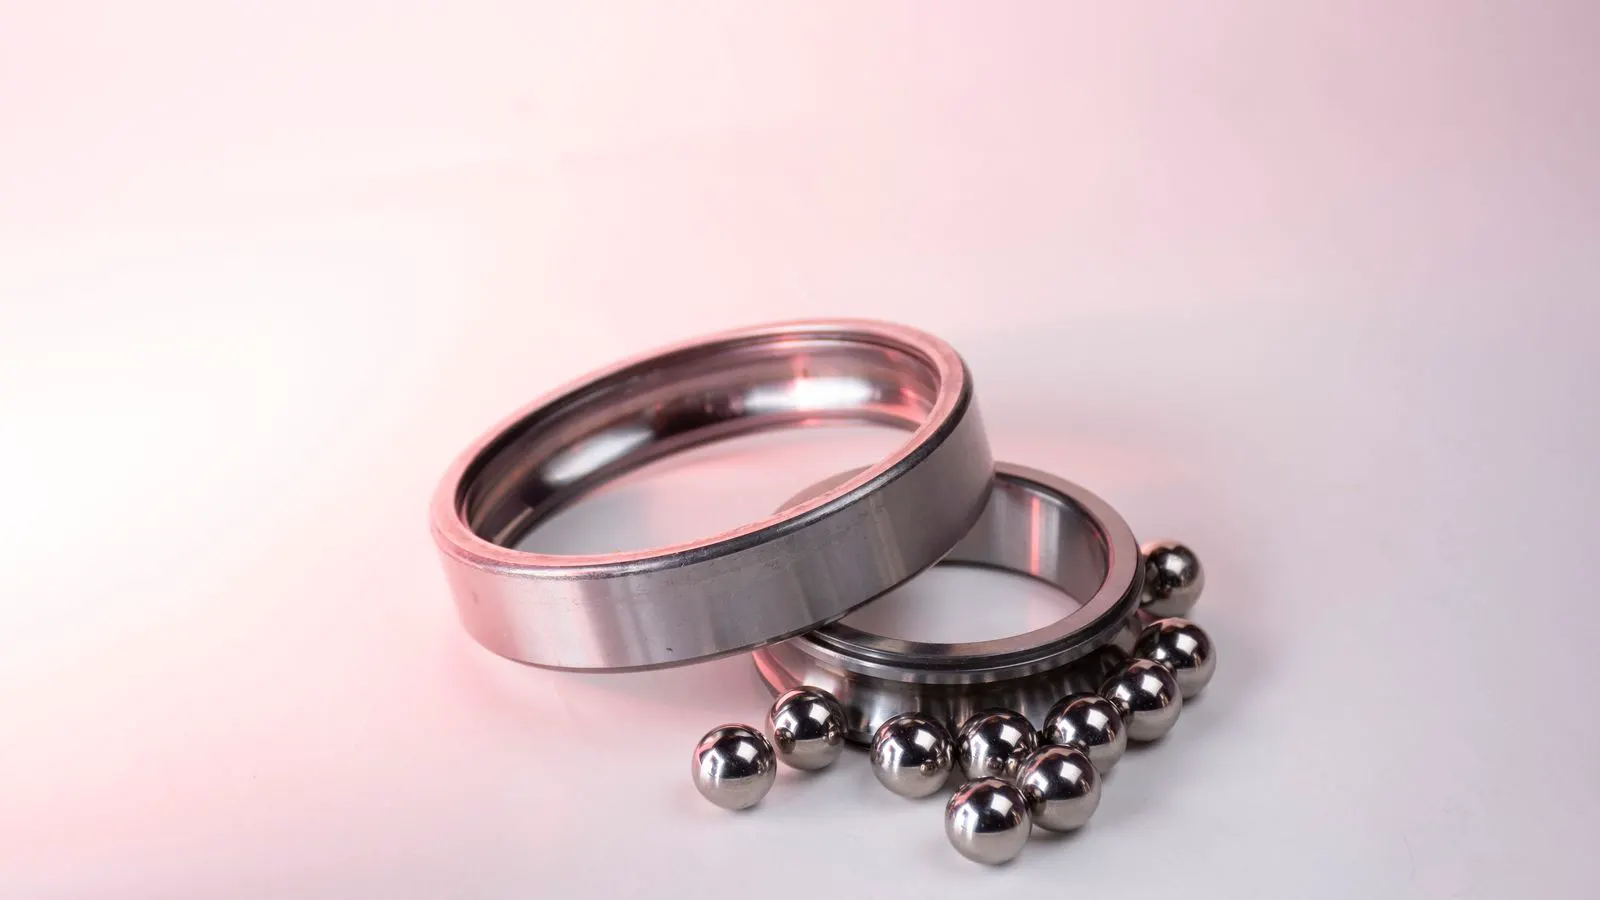
Correct O-ring installation in high-pressure systems requires careful groove preparation, material handling, and controlled assembly. Metal O-rings demand specific torque and alignment to prevent leakage and mechanical failure. This guide covers the technical steps to ensure a durable, pressure-tight seal.
- Metal O-rings require precise alignment in grooves to avoid eccentricity and pressure leaks.
- Groove surface finish and dimensional tolerance directly affect seal performance under load.
- Torque values must match the gasket material and thread type to prevent over-compression or loosening.
- Pre-installation inspection of the sealing face and groove prevents immediate failure.
- Final pressure testing confirms the integrity of the high-pressure sealing assembly.
Why Standard Rubber O-Ring Methods Fail on Metal Seals
Metal O-rings behave differently from standard elastomeric seals. They do not rely on elastic recovery to fill micro-voids. Instead, they depend on precise geometric contact and controlled deformation. Using standard O-ring installation techniques often leads to premature failure in high-pressure applications. The assumption that a metal ring will stretch like rubber is a dangerous misconception for engineers and technicians.
The primary difference is material behavior. A standard rubber O-ring can compress by 25 to 35 percent and still maintain a seal. Metal O-rings typically require much less compression, often in the range of 5 to 15 percent. Exceeding this limit causes permanent set or stress cracking. When a technician over-tightens a flange using rubber O-ring logic, the metal seal does not stretch. It thins, cracks, or loses its ability to maintain flat contact against the mating surface.
High-pressure sealing demands a different approach. The seal must withstand cyclic loading without losing its shape. If the O-ring is installed crooked or the groove is damaged, the pressure path opens almost instantly. The metal seal acts as a mechanical gasket rather than an elastomeric cushion. This changes how the seal responds to thermal expansion and pressure spikes.
Preparing the Groove and Sealing Surface
Before touching the O-ring, inspect the groove and the mating surface. The groove should have clean, unchipped edges. Any burrs or sharp corners will cut the metal seal during assembly. A small burr that might be ignored on a rubber seal will slice through a thin metal ring.
Check the surface finish. A smooth finish reduces friction during installation and helps the metal O-ring seat evenly. Rough surfaces create high stress points that weaken the seal over time. For critical pressure boundaries, the surface finish often needs to be polished or lapped.
Measure the groove width and depth. The O-ring must fit with slight clearance. Too much clearance allows movement. Too little clearance causes binding and uneven compression. Use a micrometer or feeler gauge to verify these dimensions. The tolerance is usually tighter than that for elastomeric seals.
Clean the area thoroughly. Oil, dust, or old seal residue prevents the metal O-ring from seating properly. Use a solvent that will not damage the base metal of the pressure vessel or flange. Isopropyl alcohol or a specific degreaser is usually sufficient. Ensure the area is dry before installation.
Selecting the Correct O-Ring Material and Size
Match the O-ring material to the operating medium and temperature. Metal O-rings are often made from stainless steel, nickel alloys, or molybdenum. Each material has different strength and corrosion resistance. A standard 300-series stainless steel ring may fail in a sulfide-rich environment, while a nickel alloy will hold up.
Verify the cross-section dimensions. The O-ring must match the groove profile exactly. A mismatched cross-section creates uneven contact and leaks. The cross-section determines how the metal deforms under load. A slightly larger cross-section may seem like a good fit, but it increases the torque required and risks cracking the metal.
Consider the pressure rating. High-pressure sealing requires a material that maintains structural integrity at elevated temperatures. If the system operates near the material limit, select a higher grade alloy. The heat generated during operation can change the mechanical properties of the metal.
Keep spare O-rings on hand. Metal seals can be damaged during installation. Having the correct size ready prevents delays. It is better to replace a compromised seal than to risk a leak in a critical system.
Installing the Metal O-Ring Without Damage
Handling the O-ring requires care. Metal O-rings are thin and can bend permanently if handled roughly. Use clean, dry hands or nitrile gloves. Avoid steel tools that can scratch the surface. Scratches create stress concentrations that lead to fatigue failure.
Orient the O-ring correctly before placement. Many metal O-rings have a specific direction for installation, especially in flange or gland configurations. Reversing the part can prevent proper sealing. Some designs have a raised edge or a specific groove alignment that must face the correct direction.
Slide the O-ring into the groove gently. Do not force it. If it binds, stop and inspect the groove for obstructions. Forcing the seal causes distortion. The metal will not recover from this deformation.
For threaded connections, use a thread sealant only if specified by the manufacturer. Some metal O-rings require dry installation. Adding the wrong compound can clog the seal path. If a sealant is required, apply it only to the threads, not the sealing surface.
Controlling Torque and Compression During Assembly
Torque control is the most critical step in industrial O-ring setup. Over-torquing compresses the O-ring beyond its safe limit. This creates high stress and can cause the metal to crack under pressure. The goal is to achieve the specified compression without exceeding the yield strength of the metal.
Use a calibrated torque wrench. The torque value depends on the thread size, material, and required compression. Refer to the equipment manufacturer’s data for the exact specification. If the specification is not available, consult the material datasheet for the yield strength and calculate the required torque.
If a torque specification is unavailable, use the manufacturer’s recommended range. Start with the lower end of the range. Tighten in stages, adding a small amount of torque at each step. This allows the seal to settle into the groove evenly.
Check for even seating. The flange or housing should close uniformly. If one side closes before the other, the O-ring will be compressed unevenly. This creates a weak point. Use a torque sequence, such as a star pattern, to ensure uniform compression.
Verifying the High-Pressure Seal
After assembly, verify the seal before pressurizing the system. A visual inspection looks for leaks at the flange or gland. Use a leak detection fluid if the system operates at low pressure initially. This method can reveal small leaks that might not be visible to the naked eye.
Perform a pressure test. Ramp up the pressure slowly to the operating level. Monitor for pressure drop. A stable reading confirms the seal is holding. Do not increase the pressure too quickly. The metal seal needs time to settle.
Check for movement. The O-ring should not shift within the groove under load. If it does, the compression was too low or the groove was too wide. This movement can lead to fatigue failure over time.
If a leak appears, disassemble and inspect the O-ring. Metal seals are often single-use. If the O-ring shows deformation, damage, or discoloration, replace it. Do not attempt to reuse a compromised seal. Even minor damage can lead to a catastrophic failure.
Common Installation Mistakes to Avoid
The following mistakes cause most O-ring installation failures in high-pressure systems.
| Mistake | Consequence | Prevention |
|---|---|---|
| Crooked placement | Uneven compression and leakage | Use alignment guides and verify seating before tightening |
| Excessive torque | Permanent metal deformation | Use calibrated wrenches and follow torque specs |
| Groove damage | Groove cuts the seal | Inspect and deburr grooves before installation |
| Wrong material | Corrosion or strength loss | Match material to medium and temperature |
| Reusing damaged seal | Immediate or delayed failure | Replace O-ring if any deformation is visible |
Crooked placement is the most frequent error. The O-ring may appear seated, but one edge is compressed harder than the other. Under pressure, the loose edge lifts. The seal fails immediately.
Excessive torque is the second major cause. Metal O-rings have a narrow tolerance for compression. If the torque is too high, the metal thins or cracks. The seal fails before the system reaches its pressure limit.
Groove damage is often missed. Old burrs or scratches from previous maintenance can cut the O-ring. Always inspect the groove with a magnifying lens or a clean fingertip. A single burr can cut through a thin metal ring.
Wrong material selection leads to long-term failures. A steel O-ring in a corrosive environment may rust and lose its seal. The seal may work initially, then fail after weeks or months. This is why material selection is so critical.
Reusing damaged seals is a cost-saving measure that rarely works. If the O-ring was exposed to high heat or pressure, its structure has changed. It will not perform the same way on the next cycle.
Final Checks Before Start-Up
Before returning the system to service, perform a final walk-around check. Ensure all fasteners are tight and the area is clean. Remove any tools or debris from the workspace.
Review the torque values against the maintenance log. Record the actual torque used. This data helps diagnose future issues if the seal fails.
Confirm the O-ring is the correct part number. A mix-up between similar sizes is a common error in high-volume maintenance.
If the system has been idle for a long time, expect some initial leakage. Metal O-rings may need a short stabilization period to settle into the groove. Monitor the first few cycles closely.
O-ring installation is a precise task. Small errors in groove prep, alignment, or torque lead to leaks and downtime. Following these steps ensures the high-pressure seal performs as designed.
Frequently asked questions
Can I install a standard rubber O-ring in a metal O-ring groove?
No. The cross-sections and compression requirements differ. Using a rubber O-ring in a metal groove can cause improper seating and leakage under high pressure.
What is the safe compression range for metal O-rings?
Typically 5 to 15 percent. Exceeding this range causes permanent deformation and reduces the seal life.
Do metal O-rings require lubrication during installation?
Usually no. Most metal O-rings are installed dry. Check the manufacturer's instructions, as some applications may require a specific dry film or lubricant.
How often should I inspect the O-ring?
Inspect during every maintenance event or before pressure testing. Replace if any deformation, discoloration, or damage is visible.
What happens if I over-torque a metal O-ring?
The metal deforms permanently or cracks. The seal loses its shape and will leak, often immediately after pressurization.